Filter Cloth Supplier — Production Chain and Testing
Precision weaving, finishing and fabrication for demanding industrial filtration applications. There is no stock catalogue of widths.
What we build to order — and what we will not take on
"We can make all specifications" is a sentence with no evidence behind it. This is the real envelope. The last group is the one that makes the rest of it worth reading.
Machine families
- Rubber-belt horizontal vacuum belt filter Confirmed per enquiry
Core family. Endless belt with clipper, PAD or spiral joint and a finished edge.
What decides it Brand and model, measured width and developed length, a photograph of the joint.
- Vertical / tower / stacked pressure filter Confirmed per enquiry
Core family. Endless low-elongation zigzag loop.
What decides it Plate dimensions or filtration area, plus the cloth you are replacing.
- Drum, disc, leaf or chamber press Engineering review
Not our default family. We ask what machine you run before saying anything about cloth.
What decides it The machine family, confirmed first.
- Indexing / tray vacuum filters Not offered
Different cloth mechanics. We will tell you so rather than sell you a belt that does not fit.
Cloth construction
- PET and PP Confirmed per enquiry
The two polymers most belt duties are built in.
What decides it Liquor pH, temperature and cleaning chemistry.
- PA, PPS, PVDF, PTFE Engineering review
Available as a direction where the duty genuinely needs them. Cost and lead time are the constraint.
What decides it Whether the duty actually needs them rather than PET or PP.
- Monofilament, multifilament, mono+multi Confirmed per enquiry
Chosen with the weave as a single decision, not two.
What decides it Particle size, and whether release or clarity dominates.
- Staple / spun yarn Engineering review
More usual on pressure filtration than on vacuum belt.
What decides it Machine family and retention target.
- Plain, twill, satin, double and multi-layer weave Confirmed per enquiry
Double layer is the usual answer on heavy belt duties — a fine face on a coarse structural back.
What decides it Strength and retention requirements together.
Dimensions
- Belt width Confirmed per enquiry
Rubber-belt machines commonly run to about 4.5–4.8 m.
What decides it Your machine. Our own maximum loom width is being confirmed in writing.
- Developed length / circumference Confirmed per enquiry
Measured as the developed length, not as a roller centre distance.
What decides it Your machine and its take-up range.
- Filtration area, pressure filters Confirmed per enquiry
Set by plate size and plate count.
What decides it Plate size and chamber count, or the machine model.
Fabrication
- Clipper, PAD / welded and spiral joints Confirmed per enquiry
Matched to the construction your machine is already set up for.
What decides it A close-up photograph of the existing joint, both faces.
- Sewn overlap joint Engineering review
Least common on vacuum belts. We ask before proposing it.
What decides it Machine and duty.
- Edge: cut and sealed, hemmed, reinforced band, coated band Confirmed per enquiry
The usual answer when a belt keeps failing at the edge while its body is still sound.
What decides it Photographs of both edges and of the machine edge seal.
- Guide / tracking profile Engineering review
Only where your machine is built to take one. Fitting one otherwise causes the fault it was meant to prevent.
What decides it A photograph of the belt underside and the guide rail.
Operating envelope
- Temperature and pH Engineering review
The polymer is selected so your duty sits inside its envelope, not at its edge.
What decides it Normal and peak temperature, and the cleaning pH as well as the operating pH.
- Specific chemical species Engineering review
Assessed per species, not per industry label. Fluoride, chloride, oxidisers and solvents each behave differently.
What decides it What is actually in the liquor, including trace species you consider minor.
What we do not do
- Filters, frames and rubber transporter belts Not offered
We make filter cloth. We are not an equipment manufacturer, and the rubber transporter belt is a different factory.
- OEM spare parts Not offered
Independent replacement cloth — not an OEM spare part. Dimensions and construction are confirmed per enquiry.
- Quoting from an industry name alone Not offered
Two plants in the same industry run different slurries through different machines. We ask which.
Eleven stations from yarn to crate
Each station says what is controlled there and what it changes about the finished cloth. This page names the parameters; it does not quote values, because the values belong to your order.
-
Yarn and material preparation
The filament type, its diameter and the way it is wound are settled before anything reaches a loom.
Why it matters Sets the ceiling on what the finished cloth can do. No amount of finishing recovers the wrong yarn.
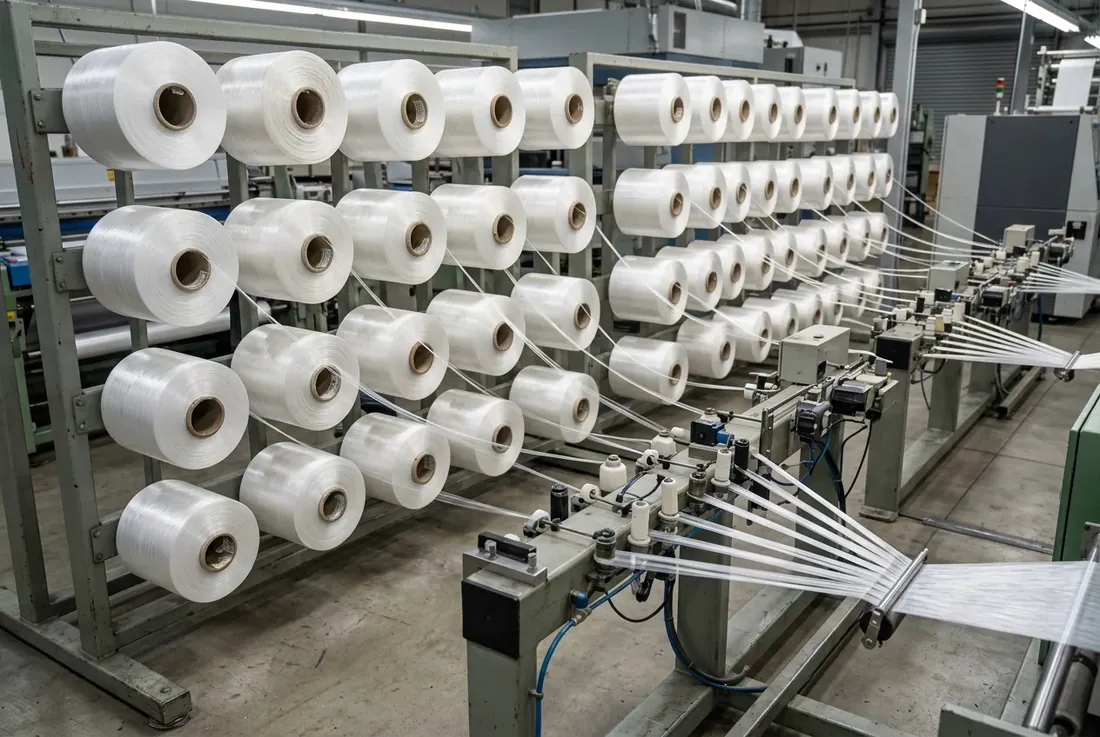
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Warping
Thousands of warp ends are wound onto a beam at even tension.
Why it matters Uneven warp tension shows up later as a belt that will not track straight.
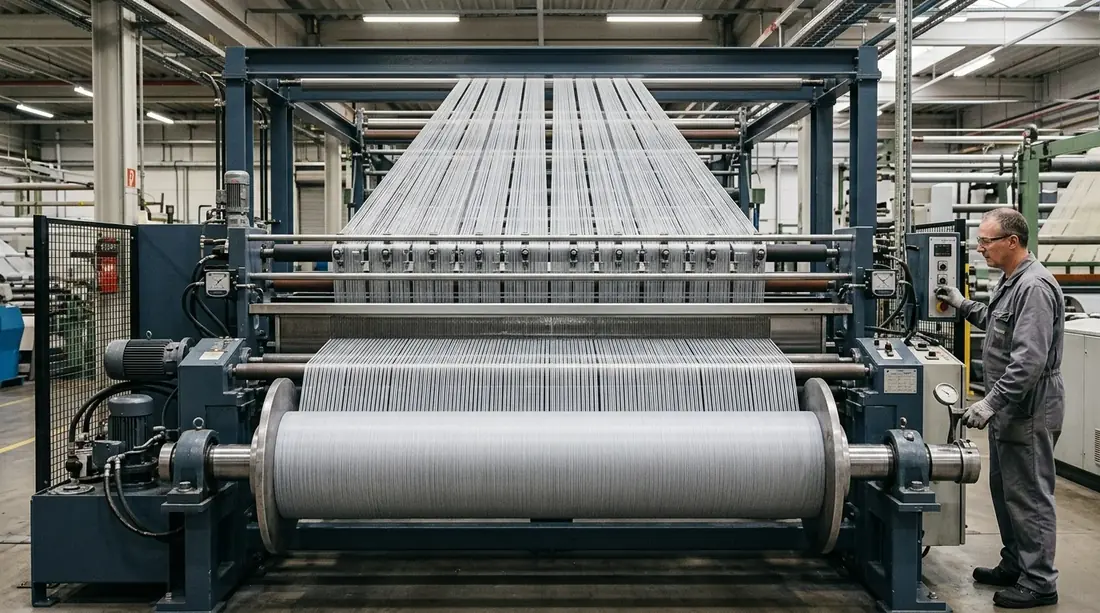
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Precision weaving
Yarn becomes the fabric structure specified for the duty — the weave, the densities, the layer count.
Why it matters Sets the balance between filtrate clarity, permeability and resistance to blinding.
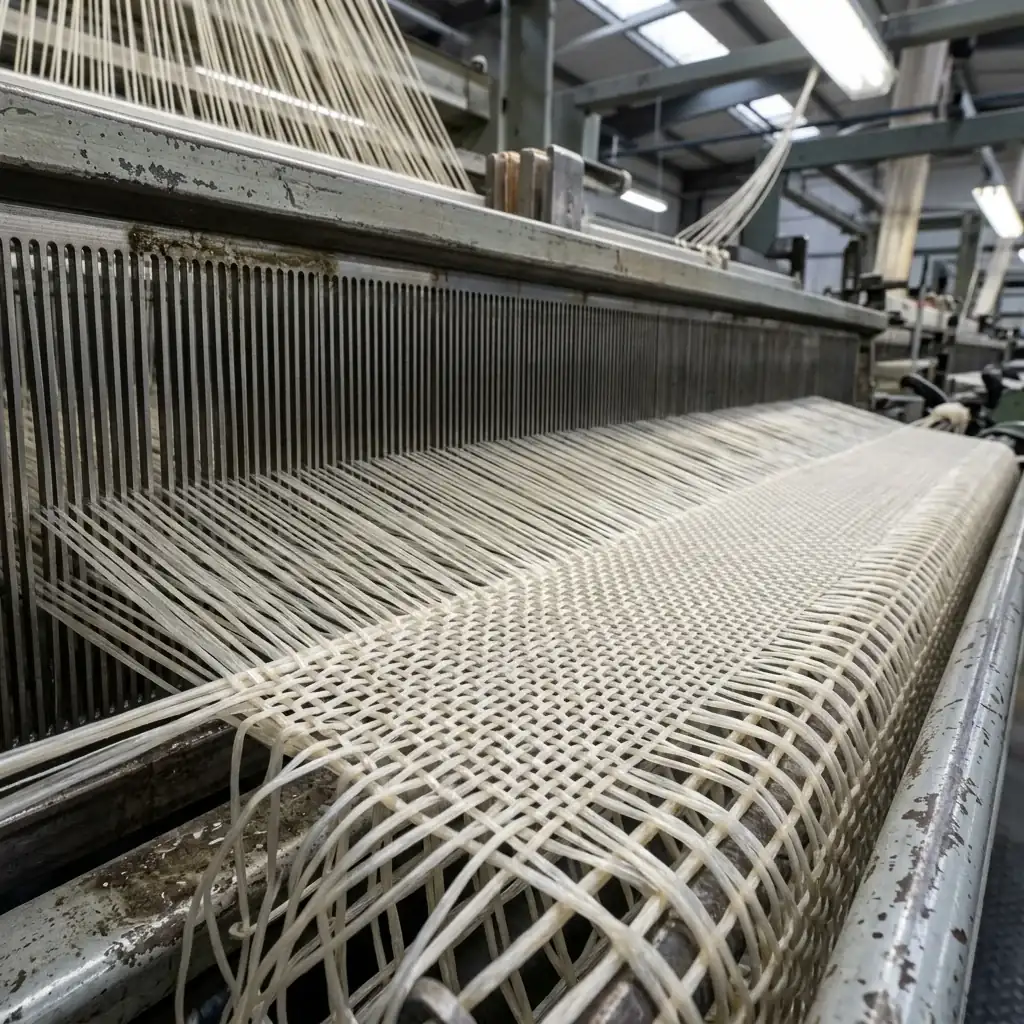
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Heat setting
The woven fabric is taken through a controlled thermal cycle under tension.
Why it matters Locks dimensions. On a tensioned endless belt this is not optional — an unset cloth changes length on the machine.
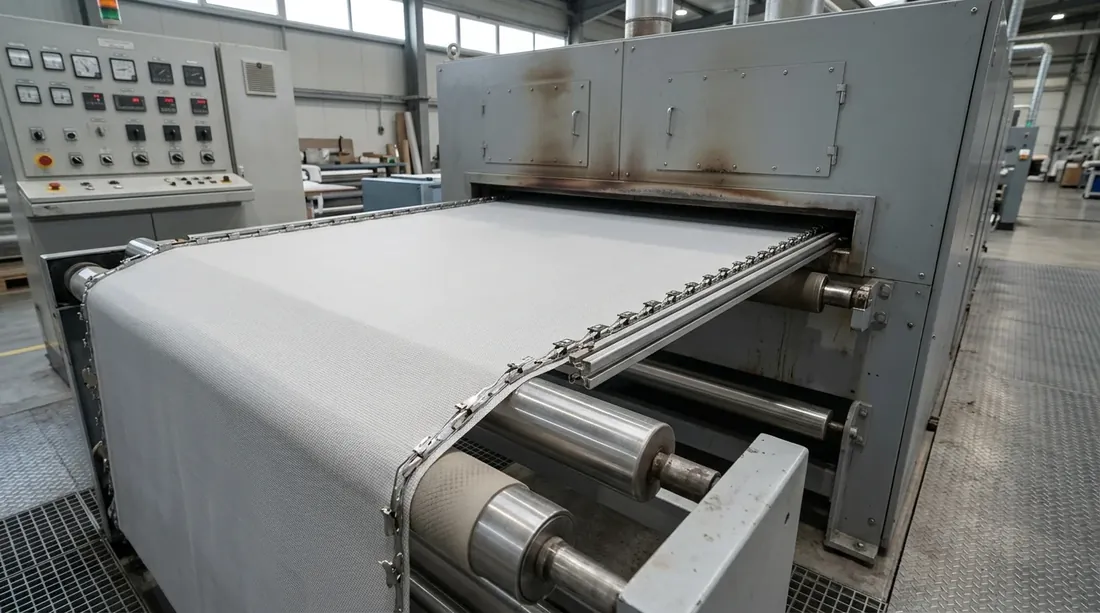
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Calendering / surface treatment
The fabric passes between heated rollers under pressure, on one face or both.
Why it matters Flattens the surface, reduces permeability in a controlled way and improves cake release.
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Cutting
The fabric is cut to the width and developed length confirmed per enquiry.
Why it matters Squareness matters as much as the nominal dimension. An out-of-square belt is a tracking fault before it is anything else.
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Joint / seam processing
The joint construction is confirmed per enquiry.
Why it matters The joint is where the belt carries its load and where it loses its vacuum seal.
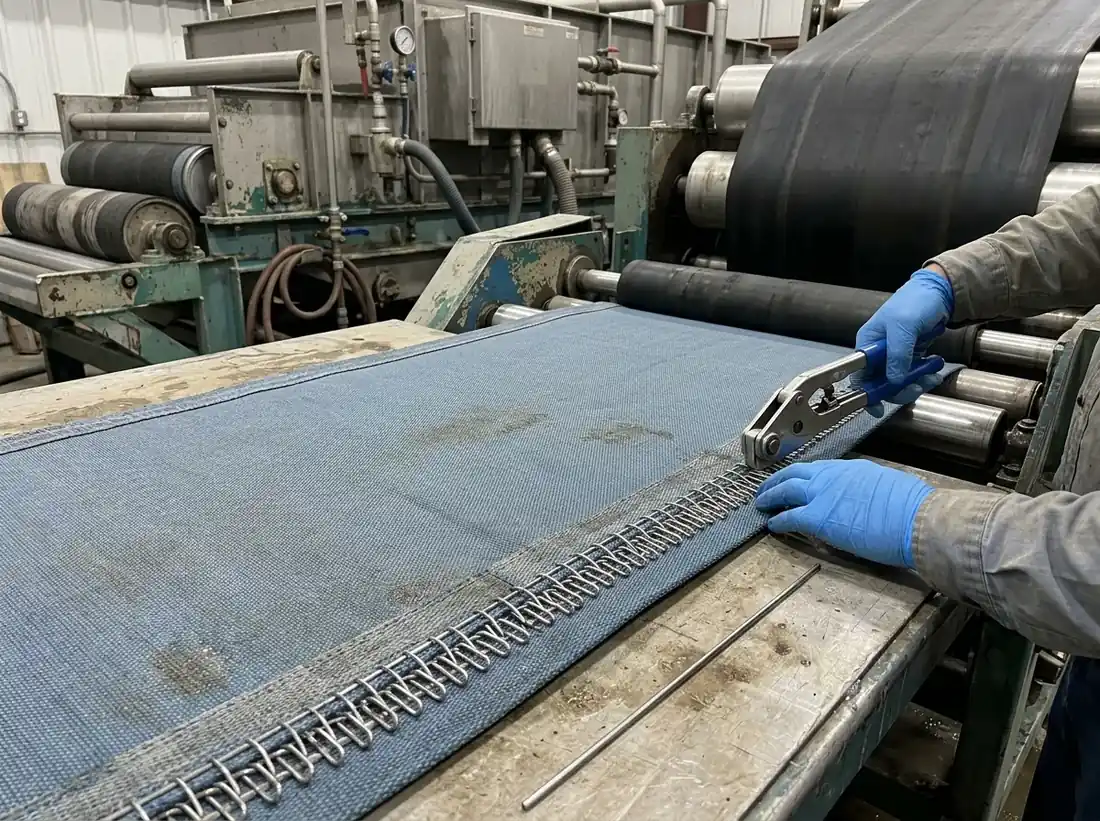
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. 
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. 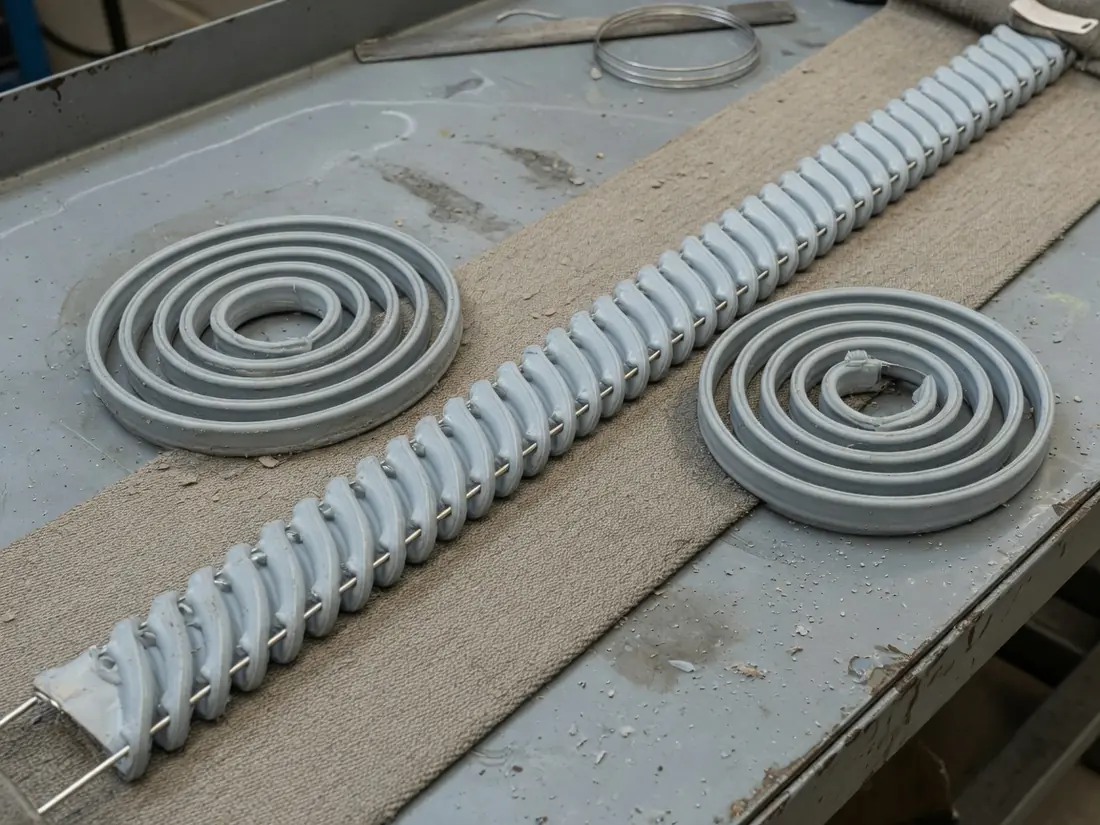
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Edge treatment
The edge finish is confirmed per enquiry.
Why it matters The edge is the highest-stress zone on a belt filter.
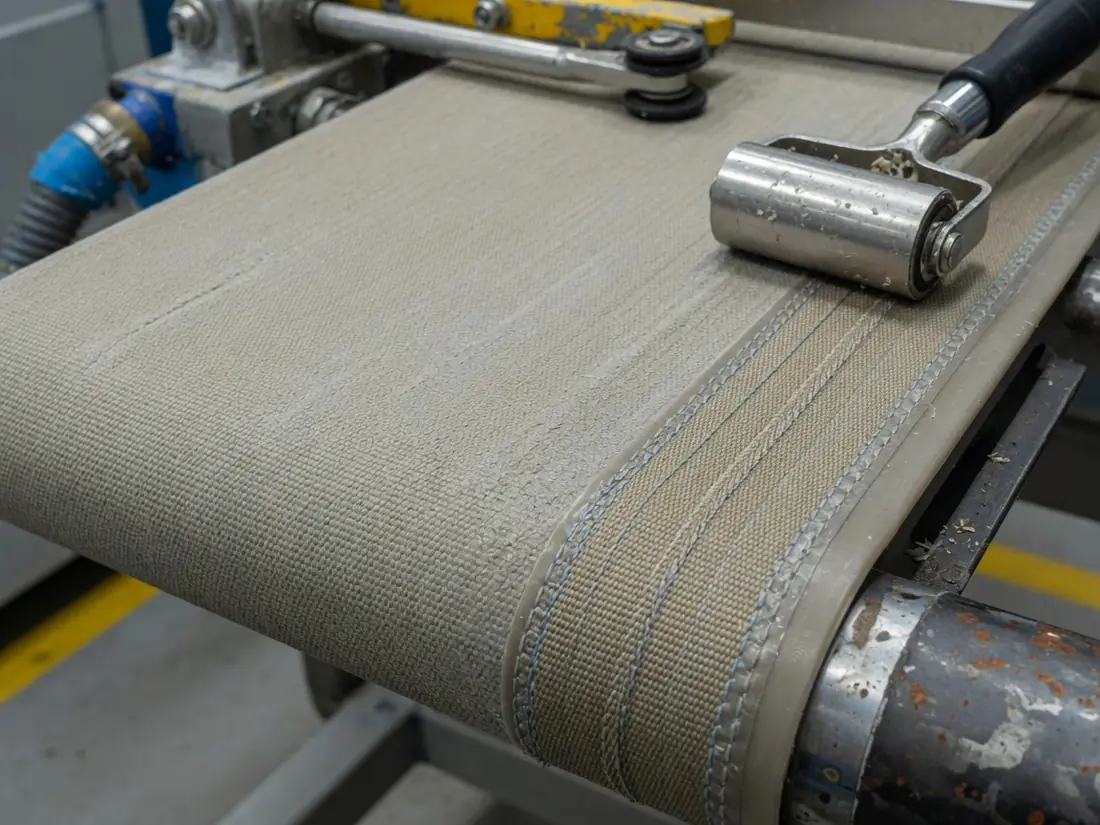
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Inspection
The full width is drawn across a backlit frame.
Why it matters Backlighting is how weave faults and contamination become visible across a full width.
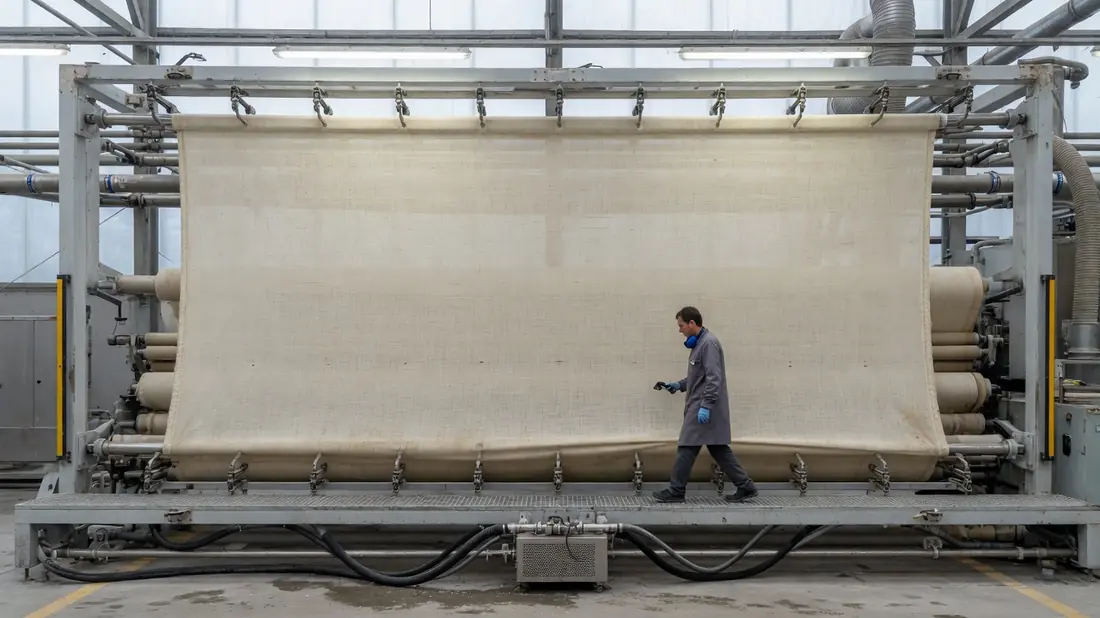
Process illustration only — representative technical-textile manufacturing, not an authentic facility view. -
Laboratory testing
Air permeability, tensile, thickness, weight and dimension checked against the agreed specification.
Why it matters A figure without its test method and test pressure is not a specification.
-
Packing and export
Rolled, wrapped and crated, labelled with your machine reference.
Why it matters A belt several metres wide is a freight problem as much as a manufacturing one.
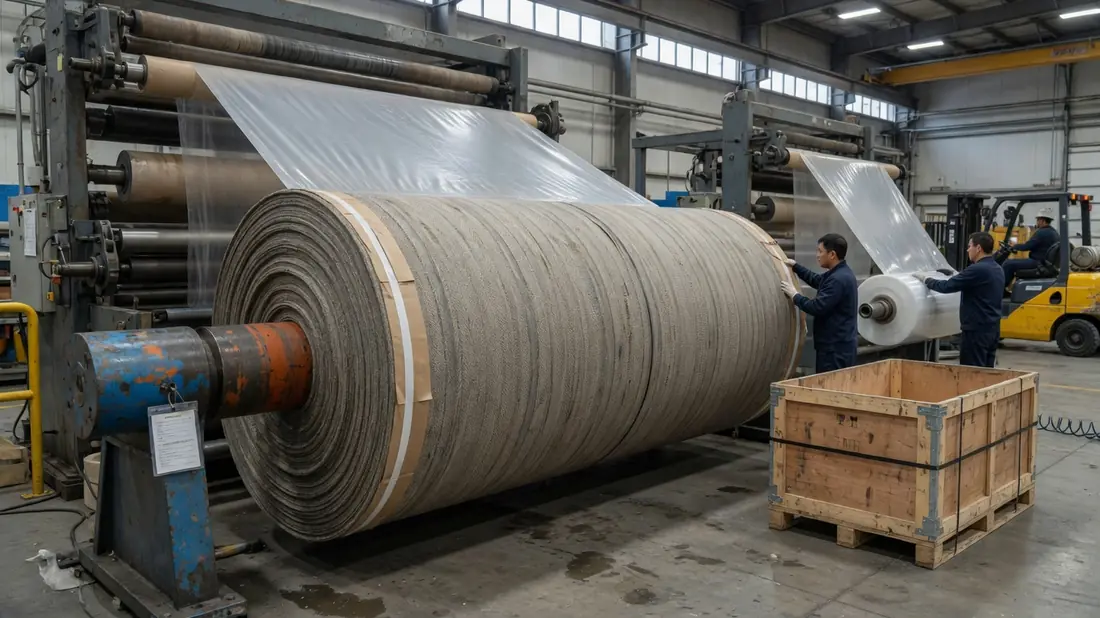
Process illustration only — representative technical-textile manufacturing, not an authentic facility view.
What gets measured, and what to ask about each figure
A test result without its method is not a specification. Each row below says what the test actually measures and the question worth asking about it — of any supplier, including us.
Air permeability
How open the cloth is, measured as airflow through a clamped sample at a stated pressure drop.
Worth asking Always ask for the test pressure and the unit alongside the number. Without both it is not comparable to anything.
Tensile strength
Breaking force, measured separately in the warp and the weft direction.
Worth asking On a belt the weft direction usually governs, so a single combined figure hides the one that matters.
Elongation
How much the fabric extends under load before it breaks.
Worth asking On a tensioned endless belt this is what decides whether it stays inside the machine take-up range.
Thickness
Measured under a stated pressure, because a compressible fabric reads differently under different feet.
Worth asking Ask what pressure it was measured at.
Mass per unit area
Fabric weight in g/m².
Worth asking An output of the construction rather than something specified on its own.
Dimensional check
Width, developed length and squareness across the finished belt.
Worth asking Squareness is the easiest of the three to leave unchecked, and it is the one that drives tracking.
Surface and weave inspection
Backlit inspection of the full width for weave faults, contamination and finish defects.
Worth asking Ask whether it is done across the full width or on samples.
Joint inspection
Alignment, squareness across the joint, and the absence of a step in thickness.
Worth asking The joint carries the load and the seal; it deserves its own check.
Edge inspection
Edge finish continuity and reinforcement along the full length.
What is documented, and what is still being documented
Everything on this page describes how the cloth is built and what each step controls. That part is settled and does not depend on paperwork.
Two things are not published yet, and we would rather name them than let you assume: photographs of our own lines, and our own confirmed parameter ranges. Production photography is being shot. Our own parameter values will be published when the mill confirms them in writing.
Until then this page carries the process in writing, and every parameter table on this site shows an honest blank rather than a plausible number.
Stock photography standing in for our floor. Images taken from other suppliers' sites. AI-generated pictures presented as our equipment. Plant age, line counts or output tonnage we cannot evidence. Certification logos without the certificate behind them.
Send the machine, not just the material
The fastest route to a correct quotation is the machine brand and model, the measured belt width and developed length, and photographs of the old cloth, its joint and both edges.