FGD Gypsum Filter Cloth for Horizontal Vacuum Belt Filters
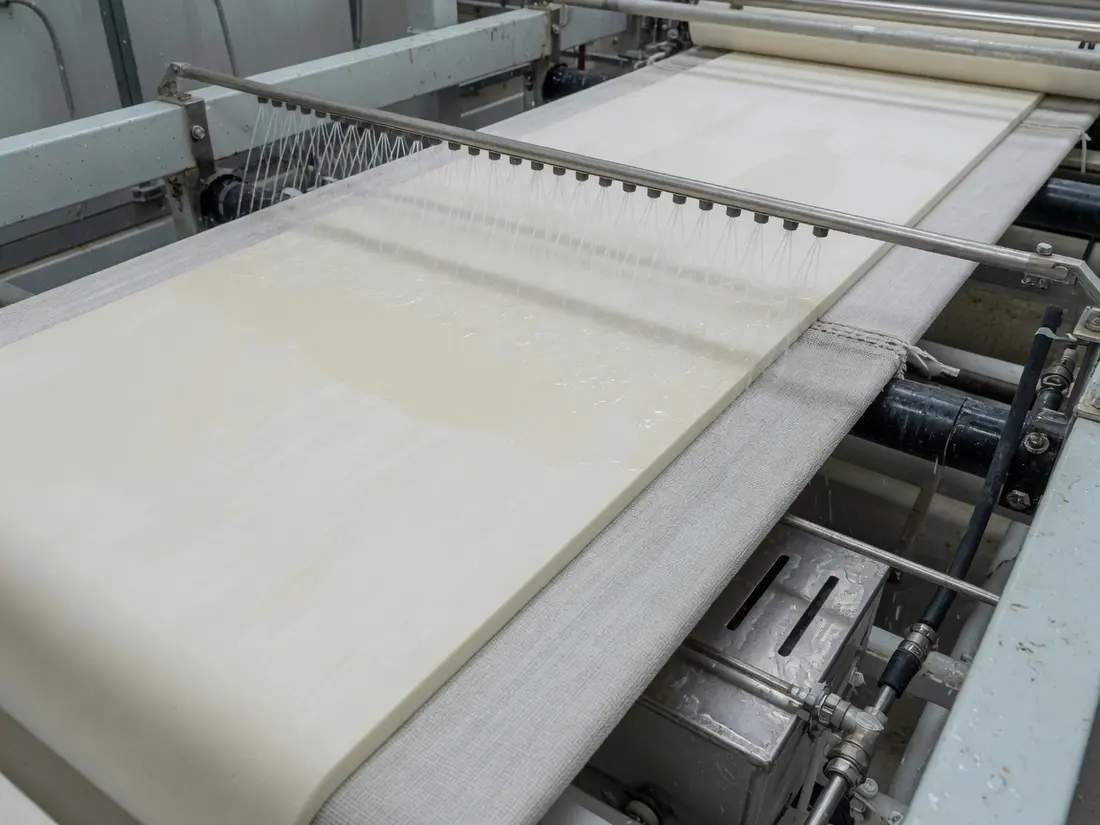
FGD gypsum is the by-product gypsum recovered from wet limestone flue-gas desulphurisation scrubbers. It is commonly dewatered on rubber-belt horizontal vacuum belt filters, where the filter cloth is a consumable endless belt.
Scrubber gypsum, and why it is its own duty
FGD gypsum is precipitated in a wet limestone scrubber: sulphur dioxide from the flue gas is captured in a limestone slurry, oxidised, and comes out as calcium sulphate. The scrubber bleed is thickened or cycloned and then dewatered, and on many plants that final dewatering step is a horizontal vacuum belt filter.
Two things make the belt a production asset rather than a piece of housekeeping. The scrubber cannot run its water balance without taking gypsum out, so a belt in trouble is a limit on the scrubber. And the cake's value — whether it is sold or landfilled — is decided on the belt, in the wash stage, not downstream.
The cloth is a consumable: an endless belt running on the grooved rubber transporter, and replaced on a cycle that your duty sets.
Same chemical family, different duty. This gypsum comes out of a scrubber and carries chlorides from the scrubber circuit; phosphogypsum comes out of a phosphoric acid plant and brings fluoride with it. At least one established weaver publishes separate belt classes for the two duties rather than a single gypsum belt, and this site keeps them apart for the same reason.
Phosphogypsum vs FGD gypsum →Process flow across the belt
- 01 Slurry Feed Scrubber bleed, usually thickened or cycloned, is fed onto the moving cloth.
- 02 Filtration Vacuum pulls scrubber liquor through the cloth and the gypsum cake forms.
- 03 Washing Wash stages displace scrubber liquor and the chlorides it carries out of the cake.
- 04 Dewatering A dry-vacuum zone pulls the cake down towards its handling moisture.
- 05 Cake Discharge Cake releases at the discharge roller for stacking, landfill or sale.
Stage-by-stage operating values — slurry solids, temperature, wash ratio, residual moisture — are plant-specific. We do not publish typical figures for them; they are on the confirmation list below.
If your gypsum has to meet a wallboard specification
On a lot of plants the person who cares most about the filter belt is not in the power station at all — it is the gypsum or wallboard company that takes the cake.
When the by-product is sold rather than landfilled, it stops being waste handling and becomes a product with an acceptance specification behind it. Chloride carry-over is the term that tends to be negotiated hardest, alongside free moisture and purity, because chlorides ride in with the scrubber liquor and the only place on the plant that removes them is the wash stage of the belt filter.
That is what puts the filter cloth in the middle of a commercial conversation. Cake that cracks washes badly; cake that washes badly carries liquor; liquor carries chloride. A cloth chosen only for filtration rate can hit throughput and still fail the acceptance test at the wallboard plant.
We do not publish a chloride limit, a moisture figure or a purity claim. Your limit comes from your off-take specification, not from us. Send us the number you have to hit and the wash configuration you run, and we will work the cloth question backwards from it.
The acceptance specification you are held to, the wash stages currently on the machine, the machine brand and model, and a recent analysis of the cake as it leaves the belt. If the plant that runs the filter is a different company from yours, say so — the answer often involves both of you.
What makes this duty hard on a belt
The liquor is chloride-bearing because it comes out of a scrubber circuit, and the wash stage carries commercial weight. Polymer and finish are chosen against that chemistry; the temperature and chemical window is confirmed in writing for your duty rather than published here as a general figure.
-
Wash efficiency, not just filtration
Wash water channels through cracks in the cake instead of displacing liquor evenly across the belt.
Cloth implication: Cake formation behaviour — which is a weave and finish question — decides whether the wash stage can do its job at all.
-
Blinding by fines and scale
Free area closes as fines and precipitated solids lodge in the fabric; throughput drifts down before anything visibly fails.
Cloth implication: Weave geometry and surface finish set how fast the fabric closes and how much of it recovers on cloth wash.
-
Tracking and wrinkling
The belt wanders on the grooved rubber transporter, contacts the edge guides and the vacuum seal starts leaking.
Cloth implication: Fabricated length, seam squareness and edge treatment all feed into tracking.
-
Seam and joint leakage
A clipper or PAD joint opens, vacuum drops as the joint crosses the box, and the cake wets back.
Cloth implication: Seam type is a specification to be decided against your machine, not a shop default.
-
Cake sticking at discharge
Cake does not release cleanly at the discharge roller and carry-over builds on the return run.
Cloth implication: Surface finish and calendering change release behaviour.
These are the difficulties common to horizontal vacuum belt duty. Which of them bites on your machine depends on numbers we do not have yet — that is what the confirmation list is for.
The machines this duty actually runs on
Horizontal vacuum belt filters are common on FGD gypsum, and they are not the only route. The families below are machine families you can enquire about for FGD service.
| OEM family | Industries listed | Next step |
|---|---|---|
| FLSmidth EIMCO Extractor | FGD, minerals | Send brand + model |
| Compositech T-REX / Chemifilter | FGD, chemicals (US) | Send brand + model |
| EKCP EIMCO-KCP | FGD and phosphate (India) | Send brand + model |
| Toncin DU | FGD, mining, lithium (China) | Send brand + model |
| WesTech HBF | Minerals, FGD directories | Send brand + model |
Drum filters also dewater FGD gypsum, and some plants are built that way on purpose. If your gypsum comes off a drum rather than a belt, this page does not apply to you — tell us your machine and we will say honestly whether we can help.
OEM names above are used only to identify the machine a cloth has to fit.
How the cloth is specified for this duty
Selection runs backwards from the slurry. Liquor chemistry and temperature narrow the polymer; particle size and the wash requirement narrow the weave and the surface finish; the machine fixes the dimensions, the seam and the edge treatment. The candidate polymers for horizontal vacuum belt duty are PET monofilament, PET mono/multifilament combinations, polypropylene, double- and multi-layer weave constructions, and hydrolysis- or alkali-resistant specialities.
Which of them belongs on your machine is not something a web page can decide, and a page that tells you otherwise is guessing on your behalf. On this duty the wash requirement usually carries more weight in the decision than raw filtration rate — but "usually" is not your plant, which is why the conversation starts with your data.
Specification status
Our own values are not yet confirmed in writing. Each parameter is fixed against your machine and slurry during the engineering review and stated in the quotation — not inferred from this page.
| Parameter | Value | Unit | How it is fixed |
|---|---|---|---|
| Polymer | Confirmed per enquiry | — | Confirmed against scrubber liquor chemistry |
| Weave / construction | Confirmed per enquiry | — | Confirmed against cake formation and wash duty |
| Air permeability | Confirmed per enquiry | L/dm²/min | Test method and test pressure will be stated with the value, once the mill confirms them in writing |
| Fabric weight | Confirmed per enquiry | g/m² | Reported with the value, once confirmed in writing |
| Seam type | Confirmed per enquiry | — | Confirmed against machine and seam photo |
| Edge treatment | Confirmed per enquiry | — | Confirmed against machine edge seal |
| Max fabricated width | Confirmed per enquiry | mm | Confirmed against loom and machine width |
| Continuous temperature limit | Confirmed per enquiry | °C | Confirmed per polymer and finish |
| Chemical limit (chloride-bearing liquor) | Confirmed per enquiry | — | Confirmed per polymer and finish |
Industry reference — not our specification
| Parameter | Industry reference | Unit | Source |
|---|---|---|---|
| Belt width range seen on this machine family | up to 4500–4800 | mm | Equipment-family observation, third-party machines |
This row describes the machine population, not what we can weave. Our own width limit is not yet confirmed in writing.
What we can build for this duty
Our own values are not yet confirmed in writing, and we will not fill them in with industry averages. This section sets out the options this cloth is built from, what each one changes, and which piece of your data decides it. Nothing below is a specification — it is the shape of the decision.
Cloth form An endless belt. Same cloth form as the phosphogypsum duty, different specification — the origin and the chemistry are not the same.
Recommended material direction
This gypsum comes out of a wet limestone scrubber, not an acid plant, and the species that defines it is chloride. Chloride is not what limits the polymer. It is what puts the metal in the joint in question, and what the wash train has to get out of the cake before it meets a wallboard specification.
This narrows the field; it does not pick. Which polymer goes on your machine is settled against your measured numbers and not on a web page — the same position the selection section above takes. What follows is the reasoning behind that position, not a departure from it.
- Polyester (PET) PET
Continuous reference up to ~150 °C — a published property of the polymer, not a value of ours
- Acid Good
- Alkali Limited
- Hydrolysis Limited
- Abrasion Excellent
The reference polymer for belt duties: abrasion resistance and dimensional stability under tension. Its published weak side is hot alkaline liquor, so the question to answer here is what your cleaning cycle runs at, not what the scrubber runs at.
- Polypropylene PP
Continuous reference up to ~90 °C — a published property of the polymer, not a value of ours
- Acid Excellent
- Alkali Excellent
- Hydrolysis Excellent
- Abrasion Good
Comfortable across the pH scale and indifferent to chloride. The constraint is the polymer reference temperature above, and creep under sustained load on a long tensioned belt.
- PA Polyamide absorbs moisture and changes dimension with it — an awkward property on a belt that has to hold its developed length between take-up adjustments.
What actually decides it Scrubber liquor temperature at the filter, and the cleaning chemistry. Then the cake chloride target, because it is the wash stage that has to hit it, and the wash is a cloth decision as much as a process one.
Everything in this block is reasoning from published polymer behaviour applied to the chemistry described further up this page. It is a direction, not a selection — and the selection is made against your measured numbers during the engineering review, then written into the quotation. The full polymer envelope is on the materials page.
Weave options
Wash performance is what this duty is bought on. A surface that releases the cake cleanly and washes back is worth more here than the last increment of retention.
- Double layer / multi-layer Two or more interlaced fabric layers woven as one. A fine filtering face carried on a coarse structural back — high strength with fine retention, and drainage channels inside the fabric. Watch: Thicker and heavier; more expensive to weave. The usual answer on heavy belt duties.
- Twill The crossing point steps sideways each pick, giving a diagonal rib. More flexible and more permeable than plain at the same yarn count, with better cake release. Watch: Slightly less dimensionally stable than plain.
- Satin Long floats, few crossing points. The smoothest surface of the three, so the best cake release and the easiest to wash back. Watch: Floats snag and abrade; retention is coarser at a given yarn count.
Smoother surfaces release and wash back better and retain more coarsely at the same yarn count; that trade is the whole of the weave decision on a wash-critical duty.
Yarn form. Monofilament is the direction where wash-back dominates. Multifilament buys finer retention and pays for it by holding solids inside the yarn bundle, which is the opposite of what a wash stage wants.
Yarn form, weave and surface finish are settled as one decision. Standard woven options are monofilament, multifilament and mono+multi combination; staple / spun yarn is evaluated under engineering review.
Permeability considerations
Air permeability is the figure everyone compares and the easiest one to quote meaninglessly. It is measured per ISO 9237 at a stated pressure drop — often 200 Pa — or per ASTM D737 (Frazier). A value with no stated pressure and no stated unit is not comparable to anything, including ours. The same applies to a pore or retention rating: on a woven cloth that is a nominal figure and not an absolute cut-off, because woven media do not have a single pore size and the cake quickly becomes the real filter.
A cloth that filters beautifully and washes badly fails the chloride specification, not the filtration specification. Ask for the permeability figure with its method and pressure, then ask what the wash does to it.
How each property is measured, and what to ask any supplier for alongside the number, is set out on the testing and inspection page. Naming the method is a fact about a public standard, not an assertion of completed mill testing.
Joint options
- Clipper (metal hook) Interlocking metal hooks crimped onto both cloth ends, joined by a pintle wire. Fitted and replaced on the machine without dismantling it. The fastest change-out. Watch: The joint is a discontinuity: it leaks vacuum as it passes the box, and it is where most belt failures start. Hook material has to suit the liquor.
- PAD / welded overlap The two ends are overlapped and thermally fused. A smoother, quieter joint that seals better than a clipper and carries load more evenly. Watch: Made off the machine or with a portable press; a change-out takes longer.
- Spiral Spiral coils on each end interlaced and pinned. Flexible, drains through the joint, distributes load along the full width. Watch: Adds an open line across the belt — not appropriate where the joint must seal.
Chloride-bearing liquor puts the hook material of a clipper joint in question — the metal is the chloride-sensitive part of that assembly, not the fabric. A PAD or welded overlap takes the metal out of the equation and costs a longer change-out. Send a close-up of the joint you run now, both faces.
The four constructions drawn in cross-section: how joints fail and what each one costs you.
Edge treatment
- Cut and sealed The cut edge is thermally sealed against fraying. The baseline. Adequate where the machine edge seal is in good condition.
- Folded / hemmed The selvedge is folded back and secured. Adds thickness and stiffness at the edge where the seal rubs.
- Reinforced edge band A separate band is bonded along the selvedge. For machines that chew edges — the usual answer when a belt keeps failing at the edge while its body is sound.
- Coated / sealed band A polymer band is applied to the edge. Seals the edge against vacuum bypass as well as protecting it mechanically.
- Guide strip / tracking profile A profile bonded to the underside to run in the machine guide. Only where the machine is built for it. Fitting one to a machine that is not is a common and expensive mistake.
Edge treatment and the condition of the machine edge seal are assessed together — a vacuum bypass at the edge shows up as a wet cake long before anyone blames the edge.
Edge constructions drawn in cross-section: how vacuum belt edges wear and what each treatment addresses.
Relevant equipment
A filter belt is decided at the loom before it is decided anywhere else: what a weaving platform can hold — pick density, tension, width — sets what the finished cloth can be asked to do.
Wallboard-grade duty is a dimensional argument as much as a chemical one: a belt that arrives out of square wanders, and a belt that wanders leaks vacuum at the seal.
The eleven process stations from yarn to crate and the nine laboratory checks: manufacturing.
Factory capability for this duty
The rows below are the part of our capability envelope that this duty touches. The last group is the one that makes the rest of it worth reading — a supplier who can do everything has told you nothing.
Machine families
- Rubber-belt horizontal vacuum belt filter Confirmed per enquiry
Core family. Endless belt with clipper, PAD or spiral joint and a finished edge.
What decides it Brand and model, measured width and developed length, a photograph of the joint.
- Indexing / tray vacuum filters Not offered
Different cloth mechanics. We will tell you so rather than sell you a belt that does not fit.
Fabrication
- Clipper, PAD / welded and spiral joints Confirmed per enquiry
Matched to the construction your machine is already set up for.
What decides it A close-up photograph of the existing joint, both faces.
- Sewn overlap joint Engineering review
Least common on vacuum belts. We ask before proposing it.
What decides it Machine and duty.
Operating envelope
- Specific chemical species Engineering review
Assessed per species, not per industry label. Fluoride, chloride, oxidisers and solvents each behave differently.
What decides it What is actually in the liquor, including trace species you consider minor.
What we do not do
- OEM spare parts Not offered
Independent replacement cloth — not an OEM spare part. Dimensions and construction are confirmed per enquiry.
The full envelope, including the machine families and services we decline: what we build to order and what we will not take on. Fifteen pages on how a specification like this is built and read: the filter cloth specification guide.
How FGD gypsum belts come off the machine
A failed belt is usually three-way: something in the cloth, something in the machine, and something in the process. Calling it a cloth problem straight away is the fastest route to buying the same failure twice.
Belt tracking and wrinkling
Often machine-side (roller alignment, edge guides) before it is cloth-side.
Diagnose this →Seam / joint failure
Cloth-side and fabrication-side: seam type, squareness, and how the joint was closed on site.
Diagnose this →Cloth blinding
Process-side (fines, scaling, wash balance) interacting with weave choice.
Diagnose this →Poor cake release
Cloth surface and discharge geometry together; rarely one or the other alone.
Diagnose this →Cloth life on a horizontal vacuum belt filter is duty-specific. Published third-party cases run from weeks to months depending on slurry and machine condition, and we do not quote a life figure before seeing your duty. A supplier who promises you a number of months without asking what you filter is selling, not engineering.
Measuring the old belt and photographing where it failed is the first step in telling the three causes apart. How to measure your old belt →
What we need from you to quote
Gather this before you fill in the engineering RFQ form; anything the form has no field for goes in the Message box. Each item removes a guess from the specification.
| What to confirm | How to get it |
|---|---|
| Machine brand and model | Copy it off the machine nameplate. “Unknown” is an acceptable answer. |
| Belt width | Measure the old cloth across the web, not the rubber transporter. |
| Belt length (circumference) | Measure the endless loop, or give us the machine centre distances. |
| Seam type in use now | Photograph the joint close up — clipper, PAD, or spiral. |
| Photos of the old cloth | Face and back, plus wherever it failed. This is the single most useful thing you can send. |
| What failed | Life, blinding, tracking, seam leak, cake release, or wash quality. Compare against the failure modes above. |
| Slurry temperature and pH | From the process sheet or a recent lab analysis. |
| Where the cake goes | Landfill, stack, cement, or wallboard — and the specification it has to meet if it is sold. |
Preparing a formal plant tender or commercial BOQ? Use our FGD Tender & RFQ Specification Checklist →
Before you enquire
Can the same belt run on FGD gypsum and on phosphogypsum?
Treat them as separate specifications. The two slurries come from different processes and carry different chemistry — chloride on the FGD side, fluoride on the phosphogypsum side — and the wash duty is not the same either. A belt fabricated for one may physically fit a machine on the other, which is not the same thing as being the right cloth for it. If you run both duties, send both sets of machine and slurry data and we will quote them separately.
Get an engineering quote for FGD gypsum duty
Three steps after you submit: an engineer checks what you sent against the machine, we come back for anything missing, and you get a quotation or a sample plan.
We quote per RFQ. No online checkout.
Sample availability, size, freight and lead time are confirmed per request.
Where to go next
FGD Gypsum Belt Cloth
The cloth family for this duty: weave, polymer, seam, edge and width options.
Vacuum Belt Dewatering Cloth
This duty read from the dry zone, where residual cake moisture rather than filtrate clarity sets the cloth choice.
Phosphogypsum Filtration
A different duty, not a variant of this one — acid-plant origin, fluoride chemistry.
Phosphogypsum vs FGD Gypsum
The two duties side by side, and why one belt does not cover both.
HVBF Machine List
OEM families you can enquire about, and what we need from each machine.